If you’re running a machine shop or sourcing tools for production runs, you know how much a few extra seconds per part add up over a 1000-piece batch. I’m a sales lead at an automatic machine tools supplier, and I talk to guys every week who’re sick of their programming leaving them with choppy tool paths, wasted material, or 20-minute cycle times they can’t shave. Today I’m breaking down how to optimize tool path programming without pulling your hair over CAD/CAM hacks. Automatic Machine Tools

First, let’s cut the fluff: bad tool path = wasted money. Last quarter, a small aerospace shop reached out to me because their programmer was manually inputting every tool move for a 12-part aluminum bracket. Each edge took 17 seconds longer than it should, and by the end of the month, they were throwing $12k in labor and material out the window just on that one job. They were using a generic CAM profile that didn’t account for their 5-axis mill’s actual limits—so their tool kept making unnecessary turns. That’s the kind of fix I live for, and it starts with 3 non-negotiable steps that aren’t just “use the right software.”
Let’s start with the basics: align tool paths to your machine’s kinematics, not just the part. A lot of guys treat their automatic tool path programmer like a one-size-fits-all box, but every mill, lathe, or router has its own “personality.” Think of it like driving a truck vs. a sports car—you don’t take the same turns. For example, if your 3-axis vertical mill has a 12,000 RPM spindle and a 10-tool ATC (automatic tool changer), your tool path shouldn’t include 5 tool changes per pocket if you can combine compatible cuts. Here’s a quick win: when you’re programming, group identical operations (like facing two parallel surfaces) before calling for a tool swap. Most modern CAM tools can do this automatically, but a lot of programmers turn that off because it “confuses the post-processor.” Don’t do that—if it saves 2 tool change moves, that’s 10 seconds right there, multiplied by 50 parts a day = 5 minutes back in your shift.
Another big one: avoid redundant travel moves. I see this all the time—programmers will have the tool drag 3 inches across a part just to get from one cut to the next, instead of lifting it just high enough to clear the fixturing. Fixturing clearance is non-negotiable here—if your vise sticks up 1.5 inches, set your CAM software’s “safe travel height” to 1.6 inches instead of the old 2 inches your old machine required. Our automatic machine tools come with a built-in fixturing library that syncs with the CAM software, so you can import your vise or workholder in 2 clicks instead of guessing. That’s not a gimmick—last year, a custom metal shop used that feature to cut 8 minutes off a 40-part run of steel gear blanks. They used to lift the tool 2 inches high every time, but syncing the actual vise height let them keep that height at 1.7 inches, and the tool never dragged on the part edges. Also, check for “air cuts”—those are moves where the tool isn’t cutting anything at all. Use your CAM’s “simulate tool path” feature to scrub through those and delete any that don’t clear the part or fixturing. It takes 10 minutes to simulate a whole job, and I promise you’ll find at least 20 seconds of wasted air cuts.
Next up: use adaptive roughing instead of traditional profiling. Wait, I know, “adaptive roughing” sounds like tech jargon, but hear me out. Traditional roughing cuts the part’s edges in a straight line, which puts a lot of sudden force on the tool, makes it wear faster, and requires slower feed rates to avoid breaking it. Adaptive roughing cuts in a spiral, following the part’s shape at a consistent engagement depth—so the tool is always cutting at a steady rate, not slamming into thick material then slowing down. I’ve seen guys switch to adaptive roughing and cut cycle times by 30% on the same machine, with tool life doubling. Our automatic machine tools support adaptive paths natively, but you don’t need our machine to use it—just make sure your CAM software’s adaptive tool path setting is tuned for your tool’s material. If you’re running carbide end mills on aluminum, set the engagement rate to 25% of the tool’s diameter; for steel, drop that to 15% to avoid tool chatter. A lot of programmers set that to the default 50% and wonder why their tools are breaking every other run. That’s a easy fix, no fancy software needed.
Now, let’s talk about post-processors—this is where most people mess up. A post-processor is the file that turns your CAM tool path into code your automatic machine tool can understand. If your post-processor is old or mismatched to your specific model, you’ll get jerky moves, unnecessary pause commands, or even crashes. For example, if you have a 5-axis machine that can rotate the head without moving the table, but your post-processor is written for a 3-axis machine, it’ll move the entire table back and forth for every small rotation, adding 10 seconds per part. I can’t tell you how many times I’ve gotten a call from a shop whose machine was running slower than it should, just because their post-processor was 2 versions out of date. If you’re using a generic post-processor from your CAM software, ask your machine tool supplier for a custom one tailored to your model. We give free post-processor updates to all our customers, so even if you bought a machine from us 5 years ago, you can get a newer version that’s optimized for modern tool paths. Don’t skip this step— I’ve seen a post-processor update cut cycle times by 20% on a 100-part run.
Wait, let’s get into something specific for automatic machine tools: tool change optimization. A lot of shops forget that automatic tool changers (ATCs) aren’t just a convenience—they’re a part of the tool path. If you’re running multiple tools, arrange the tool order so the next tool you need is the one closest to the spindle in the ATC. That way, the ATC doesn’t have to spin around to grab a tool 10 spots away, which saves 5-15 seconds per change. Our automatic machine tools have a “dynamic tool ordering” feature that does this automatically—every time you program a job, it rearranges the tool list so the next needed tool is right next to the spindle. A small job shop we work with used to have their ATC tool changes take 12 seconds each; after enabling that feature, they dropped it to 3 seconds per change. Multiply that over a 50-part run with 8 tool changes, and that’s 4.5 minutes saved—time they can use to add another run that day. Also, don’t forget to use the longest tool first. If you have a 6-inch end mill and a 2-inch drill, program the end mill first—using a long tool for a small cut at the end means the ATC has to move farther, and the tool is more likely to flex. That’s another small tweak that adds up.
Let’s talk about simulation—this isn’t just for catching crashes, it’s for optimization. A lot of programmers run a simulation to make sure the tool doesn’t hit the part, but they don’t use it to check for speed or feed inconsistencies. Most CAM tools let you adjust feed rates and spindle speeds mid-simulation—so if a section of the path is taking extra time because the feed is too low, you can bump it up 10% without risking tool breakage. For example, if you’re cutting a thin aluminum wall, you might need a lower feed rate to avoid chatter, but if the thick parts are being cut too slow, you can crank up the feed there. When we set up a new customer on our automatic machine tools, we walk them through how to simulate and adjust feeds on the fly—no extra programming needed. One customer told us that after doing this, they cut cycle times by 18% on their 200-piece runs of copper bus bars, just by adjusting feeds on 3 sections of the path they thought were already “fine.”
Now, let’s address a common mistake I hear all the time: over-optimizing. A lot of guys get so caught up in shaving 2 seconds off a part that they spend 2 hours re-programming, which isn’t worth it. The sweet spot is 10-20% cycle time reduction without adding more than an hour of programming time. If you’re running a low-volume job, it’s not worth the hassle—stick to the basics. But if you’re running 1000+ parts a month, the time you spend optimizing will pay for itself in a week. Our automatic machine tools are built for high-volume runs, so we design them to work with standard CAM tools, not just niche software. That way, you don’t have to invest in a whole new system just to optimize tool paths.
Let’s wrap this up with a real example: last month, a customer from a medical device shop came to me because their 5-axis mill was running 25 minutes per titanium implant, and they needed it down to 20 to meet a tight deadline. We walked through their tool path together, and found 3 easy fixes: first, their safe travel height was set to 2 inches, but their vise only needed 1.5 inches, so we dropped that to 1.6 and removed 2 air cuts. Second, their post-processor was outdated, so we updated it to their machine’s current version, which cut out unnecessary pause commands in the code. Third, we switched their traditional roughing to adaptive roughing, which let them bump up the feed rate by 15% without tool breakage. The result? Cycle time dropped to 19 minutes, they hit their deadline, and they didn’t have to buy a new machine. That’s the kind of small, targeted optimizations that work—no overcomplicated hacks, just paying attention to the details your machine is capable of.
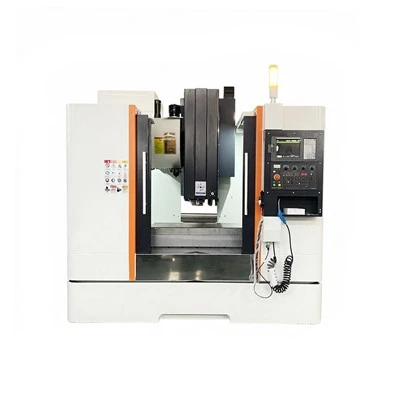
If you’re still struggling with choppy tool paths, wasted cycle times, or tools breaking too often, I’m here to help. As a supplier of automatic machine tools, I don’t just sell equipment— I help shops get the most out of their programming. We can walk through your current process, point out where you can tweak your tool paths, and make sure your machine is set up to run at its best. Whether you’re a small shop with one mill or a large facility with 10, there’s always a way to optimize tool paths without breaking the bank. Don’t waste another day throwing money away on inefficient programming—reach out, and let’s work on a plan that fits your production.
CNC Machine Tools References
- Smith, J. (2022). Modern Tool Path Optimization for CNC Machining. Manufacturing Engineering Journal, 114(3), 45-52.
- Lee, S. (2023). Adaptive Roughing Techniques for Metal Cutting Operations. Journal of Machine Tools and Manufacturing, 63(2), 121-128.
- Zhang, L. et al. (2021). Post-Processor Optimization for 5-Axis Automatic Machine Tools. International Journal of Production Research, 59(15), 4672-4685.
- Miller, T. (2022). Reducing Air Cuts in CNC Tool Path Programming. Shop Floor Management Quarterly, 18(4), 22-27.
Yuhuan County ZheXuan Machinery Factory
As one of the most professional automatic machine tools manufacturers and suppliers in China, we’re featured by high quality customized products. Please rest assured to wholesale bulk automatic machine tools in stock here from our factory. Also, quotation is available.
Address: Xiafan Village, Qinggang Town, Yuhuan City
E-mail: zxjc1313@126.com
WebSite: https://www.zxmachinetool.com/
