Hey everyone, let’s cut to the chase—if you run or manage an electrical cabinet production line, you’ve probably spent way too much time obsessing over copper busbar tightness, powder coat thickness, or PLC wiring tolerances. But how many of us actually stop to geek out over the air quality on the production floor? Spoiler: it’s not just a “nice-to-have” for dust-free desk jobs—it’s a non-negotiable for your line’s output, your team, and even your bottom line. As someone who’s worked with electrical cabinet production lines for years (no stuffy corporate title here, just been in the shop floor enough to know when a filter’s failing), let’s break down exactly what your line demands from its working environment’s air quality, no jargon overkill. Electrical Cabinet Production Line
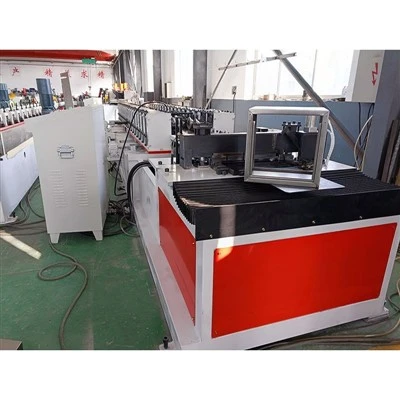
First off, let’s get specific to what we actually build: electrical cabinets. These are the ones that hold everything from circuit breakers for commercial buildings to control panels for factory robots. Every component—from the tiny surface-mount resistors to the large busbars that carry hundreds of amps—has a bad hair day when the air’s off. Let’s start with the big one: particulate matter. I’m not talking about random dust from the loading dock (though that’s bad enough). I’m talking about the stuff that’s too small to see with the naked eye but will ruin your entire production run.
Here’s the thing about electrical cabinets: most of them get sealed up once they leave the shop. If the air inside your production area has particles floating around that settle on solder joints or get stuck in powder coat before it’s cured? You’ve got a problem. For example, when we do the powder coating step—we spray a fine paint electrostatically, right? If there’s airborne lint from the nearby sewing shop (yes, that actually happened at a client’s line last year) or metal shavings from a different part of the facility, those will stick to the wet powder. When it goes through the oven, the paint cures, and now you have little craters or spots on the cabinet surface that look cheap, feel rough, and can even let moisture get in later. I’ve seen a client’s entire batch of 50 low-voltage distribution cabinets get rejected by their customer because of that exact issue—cost them $12k in scrap in one week. That’s not pocket change.
But particulate limits aren’t random. For our line specifically, we’re not in a cleanroom for microchips (thank god, those cost a fortune to run), but we’re in what’s called a Class 100,000 area—wait, no, let’s make that real. Class 100,000 means there are no more than 100,000 particles larger than 0.5 microns per cubic foot of air. Let’s put that in perspective: a human hair is about 50 microns wide, so these particles are 1/100th the size of a hair. That’s the stuff that floats around, settles on surfaces, and causes all the headaches. For cabinet lines, we need that because of two key steps: soldering and powder coating. If you’ve got more particles than that, you’re gonna have rework, delayed shipments, and angry customers.
Next up—contaminants you can’t see, or at least can’t easily spot. Gaseous pollutants. Let’s talk about volatile organic compounds (VOCs) first, but not just the ones from your paint or solvents—we also have to worry about things like hydrogen sulfide, ammonia, or even diesel fumes if your loading dock is next to the production line. Wait, why? Let’s take solder joints: when you use rosin-core solder, it melts and leaves a residue, right? If there’s hydrogen sulfide in the air (common if you’re near a wastewater treatment plant or even some food processing facilities), that will react with the solder residue over time. It causes corrosion, which makes the electrical connection worse, or even leads to arcing inside the cabinet. That’s a safety hazard—we’re not just talking about a faulty cabinet that doesn’t work, we’re talking about a fire risk. I once had a client near a port area with high sulfur levels; their control cabinets for cranes kept failing inspections because of corroded busbars, until we installed air scrubbers to pull the sulfur out. No more failures, inspections pass every time.
Then there’s humidity and temperature, which people often confuse with “air quality” but actually are super tied to it. Let’s get this straight: air quality isn’t just what’s in the air, it’s how that air behaves. For electrical cabinets, humidity is a big one. If it’s too dry (under 30% relative humidity, RH), you get static electricity. Static zap on a tiny microchip during assembly? That’s a dead component, no visual sign, so it gets shipped and then fails at the customer’s site. We call those “infant failures” and they’re the worst because you don’t catch them until it’s too late. If humidity is too high (over 60% RH), you get condensation on metal parts—rust on busbars, corrosion on screw terminals, even mold growing inside the cabinet if it’s not dried out before sealing. That’s another safety thing. Our sweet spot for cabinet lines is 40-50% RH, and temperature between 68-75°F (20-24°C). Not too hot, not too cold, air moving enough to keep humidity consistent but not so much that it blows dust around.
Wait, let’s not forget about volatile compounds from our own processes—we can’t just blame outside air. When we do the powder coating, the paint releases VOCs as it’s curing, and when we use cleaning solvents for metal parts, those evaporate too. If we don’t filter those out, they don’t just make the shop floor smell like chemicals—they can react with other components, like the gaskets we use to seal cabinets. I’ve seen gaskets swell or get brittle from prolonged exposure to leftover solvent fumes, which ruins the cabinet’s IP rating (that’s the ingress protection, for water and dust). A client had a batch of outdoor cabinets that failed a rain test because their gaskets were deformed from air full of solvent vapors—we adjusted the exhaust system and added carbon filters, and now their IP ratings stay perfect.
Another thing people sleep on: air pressure differentials. Let’s say your powder coating booth is in one section of the floor, and your assembly line is right next to it. If the booth is at a lower air pressure than the assembly area, all that paint dust and solvent fumes from the booth will leak out into the rest of the line. You can’t see it, but it’s there, settling on your unassembled circuit boards and wiring. The fix is simple: zone your line, make each high-dust/high-VOC area (powder booth, metal fabrication, cleaning stations) negative pressure compared to adjacent areas, and make the assembly and testing areas positive pressure so clean air flows in, not out. That’s a cheap adjustment compared to the rework from contaminated parts.
Now, let’s talk about why this isn’t just “compliance stuff” (though it is, by the way—OSHA has limits on workplace air quality, and electrical cabinets have industry standards like IEC 60439). This is about quality, speed, and saving you money. Let’s do a quick math check: a small cabinet line does 200 cabinets a day. If 5% get rejected due to air-related contamination, that’s 10 a day. At an average of $200 per cabinet in materials and labor, that’s $2,000 a day in scrap—$520,000 a year. Fixing your air quality system? A one-time cost of like $15,000-$25,000, and monthly filter/scrubber costs of a few hundred bucks. That’s a no-brainer.
I’ve worked with lines that ignored this stuff, and lines that took it seriously. The good ones? They keep rework under 1%, their customer satisfaction is through the roof, and they don’t have to deal with late shipments because of bad parts. The bad ones? They’re constantly putting out fires—literally sometimes, with corroded wires. And it’s all because they forgot that the air around their production line is just as important as the tools they use or the parts they assemble.
Wait, let’s make sure I’m not missing anything. What about the workers? Yeah, this isn’t just about products. If your shop floor has high levels of VOCs or dust, your team’s going to have headaches, respiratory issues, which leads to more sick days and higher turnover. A friend of mine runs a cabinet line, they added air filtration last year, and their sick days dropped by 30%—that’s a huge win for morale and productivity too.

So, putting it all together, here’s the non-negotiable air quality requirements for your electrical cabinet production line, no fancy terms:
- Particulates: Max 100,000 particles >0.5 microns per cubic foot. No random lint, metal shavings, or dust from outside blowing in.
- Gases: No excess hydrogen sulfide, ammonia, or unfiltered VOCs from your own processes. Use scrubbers and carbon filters where needed.
- Humidity/Temp: 40-50% RH, 68-75°F. Avoid static and condensation.
- Pressure Zones: High-dust/chemical areas are negative pressure, clean areas are positive pressure to keep contaminants where they belong.
Door Panel Production Line If you’re reading this and thinking “our air system feels off” or we’re having too many reworks for weird, unexplained reasons—hit me up. I’ve helped a ton of cabinet lines tweak their air quality setups to fix exactly these issues, no overpriced consultants, just real shop floor knowledge. Let’s chat about your line’s specific pain points, figure out what adjustments would work for you, no pressure, just straight talk about making your production run smoother and cheaper.
References
- International Electrotechnical Commission (IEC). IEC 60439-1: Low-voltage switchgear and controlgear assemblies – Part 1: General rules, 2020.
- Occupational Safety and Health Administration (OSHA). Indoor Air Quality in the Workplace, 2022.
- American National Standards Institute (ANSI). ANSI/ISA-71.04: Environmental conditions for process measurement and control systems, 2013.
- National Fire Protection Association (NFPA). NFPA 70: National Electrical Code, 2023.
- Society of Manufacturing Engineers (SME). Air Quality Controls for Industrial Manufacturing Facilities, 2021.
Weifang Yue Jun Machinery Co., Ltd.
With abundant experience, we are one of the most professional electrical cabinet production line manufacturers in China. We warmly welcome you to buy durable electrical cabinet production line made in China here from our factory. We also accept customized orders.
Address: Kuiwen District, Weifang City, Shandong Province
E-mail: adrian@yuejunmachinery.com
WebSite: https://www.yuejunmachinery.com/
