When I first started working in the shrink tunnels and accessories industry, I’ll admit I underestimated how much of a difference proper insulation makes. Early on, we had a customer running a 12-pack of bottled water through a shrink tunnel and complaining that their film was shrinking unevenly, leading to 15% more waste than the industry average. They tried adjusting conveyor speed, temperature settings, even switching to a different film brand, but nothing stuck. It wasn’t until our service technician pulled the back panel of their tunnel off to run a diagnostic that we found the culprit: a 2-inch gap where insulation had shifted over time, letting heat escape right through the side of the machine. That moment drove home just how critical insulation isn’t just a “nice-to-have” for shrink tunnels—it’s the backbone of consistent, cost-effective, and safe operation. Shrink Tunnels & Accessories
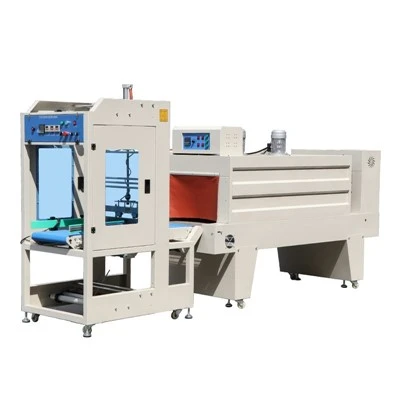
Let’s break down why that initial gap caused so many problems. Shrink tunnels work by exposing polyolefin or PVC film to controlled, uniform heat, usually between 250 and 300 degrees Fahrenheit, to make it tight and conform to the product. If insulation is compromised, the heat inside the tunnel becomes inconsistent: hot spots near the heating elements, cold zones further from the walls, and dramatic heat loss at any gaps. In that water bottle customer’s case, some packs were being exposed to too much heat, leading to burnt film and stuck labels, while others got too little heat, resulting in loose, wrinkled shrink wrap that risked tearing during shipping. That inconsistency directly translated to higher material waste, slower line speeds as operators had to stop and fix bad packs, and even higher energy bills because the tunnel’s heater had to run longer to compensate for lost heat.
Beyond just product quality, proper insulation impacts energy efficiency more than most tunnel operators realize. Energy is one of the biggest ongoing costs for any packaging line, and shrink tunnels account for up to 30% of a facility’s total packaging energy use in some operations. A 2022 study from the Packaging Machinery Manufacturers Institute (PMMI) found that shrink tunnels with worn or missing insulation can waste 25 to 40% of their heat output. That means if you’re running a 10-horsepower tunnel, you could be wasting nearly 4 horsepower just because heat is leaking out. For a small beverage operation running two shifts a day, that adds up to thousands of dollars in unnecessary energy costs annually. On top of that, uninsulated or poorly insulated tunnels force heating elements to work overtime, shortening their lifespan and leading to more frequent replacements—another hidden cost for operators.
Safety is another factor that often gets overlooked when talking about insulation. Exposed heat from a shrink tunnel isn’t just a fire risk for nearby flammable materials like shrink film boxes or cardboard product packaging; it’s a hazard for line workers. A tunnel with insufficient insulation will have surface temperatures that can reach 180 degrees Fahrenheit on the exterior, which is high enough to cause severe burns if a worker accidentally brushes the side during a line jam. Proper, well-installed insulation keeps the exterior surface temperature of the tunnel safe to the touch, reducing workplace injuries and the associated workers’ comp costs that come with them. We’ve had multiple customers who noted a drop in minor line worker accidents after upgrading their tunnel’s insulation, which is a side benefit no one expects but is incredibly valuable.
Now, not all insulation is created equal, and that’s where our role as a shrink tunnel and accessories supplier comes in. The best insulation for shrink tunnels isn’t just fluffy fiberglass—it needs to be heat-resistant, moisture-proof, and able to withstand the constant vibration of conveyor lines. Many older shrink tunnels use standard fiberglass insulation, which breaks down over time when exposed to high heat and chemical fumes from shrink film. That’s why we supply high-density ceramic fiber insulation specifically designed for packaging equipment: it can handle temperatures up to 2,300 degrees Fahrenheit, resists degradation from fumes, and has a thermal conductivity rating that keeps heat locked inside the tunnel. We also supply custom-cut insulation panels that fit perfectly into tunnel walls, gaps, and doors, eliminating the kind of spaces that let heat escape.
Regular insulation maintenance is just as important as having the right insulation to begin with. We recommend that customers inspect their tunnel’s insulation at least every six months, or more often if they run their line around the clock. Common issues include insulation shifting due to vibration, gaps forming around door seals, or moisture buildup from humid environments that breaks down insulation over time. For example, a warehouse in the Southeast US that runs food products will have higher humidity, which can cause fiberglass insulation to clump and lose its insulating value in as little as a year. Our service team often works with customers to do insulation audits, where we check for gaps, test exterior temperature, and make adjustments to ensure the tunnel is running at peak efficiency.
There’s also a direct link between insulation and shrink film compatibility. Different films require different heat levels to shrink properly: polyolefin, the most common film for food packaging, needs a more gradual heat profile than PVC. If your tunnel’s insulation is causing inconsistent heat, you can’t dial in the right profile for your film, leading to either over-shrinking that damages delicate products like glass jars or under-shrinking that leaves products vulnerable to damage during transit. One of our food packaging customers switched to a higher-quality film to meet new food safety standards, but their old tunnel’s insulation made it impossible to get a tight shrink without burning the film. After they upgraded our ceramic fiber insulation panels, they were able to adjust their heat profile perfectly, cutting film waste by 12% within a month.
Let’s talk about long-term return on investment (ROI) because that’s what matters most for any business. The cost of proper insulation is a fraction of the savings you’ll get from lower energy bills, less film waste, and fewer equipment repairs. For a mid-sized shrink tunnel, a full insulation upgrade from standard fiberglass to high-density ceramic fiber costs around $1,500 to $2,000. The energy savings alone will typically pay for that investment in 8 to 12 months, based on average industrial energy costs in the US. Add in the reduction in film waste—often 10 to 15%—and the extended lifespan of heating elements, and that ROI gets even faster. We’ve seen customers recoup their insulation costs in as little as six months when they were dealing with major heat loss.
It’s also worth noting that insulation isn’t just for new shrink tunnels. Many operators with 5- or 10-year-old tunnels don’t realize their insulation has degraded, so they’re operating at less than optimal efficiency without knowing it. We’ve had customers come to us thinking they needed a new shrink tunnel only to find out a simple insulation upgrade would fix their main issues. That’s why we always take the time to walk customers through their current setup, point out areas where insulation is lacking, and offer solutions tailored to their specific line. Whether it’s replacement insulation panels, door seals that prevent heat loss, or insulation wraps for older tunnels, we carry all the accessories needed to keep a shrink tunnel working at its best.
Another often overlooked point is product integrity for delicate items. For example, pharmaceutical products or electronics that are packaged in shrink wrap can’t handle uneven heat—hot spots can warp plastic packaging or even damage sensitive components. Proper insulation ensures that every item passing through the tunnel gets the same amount of heat, eliminating the risk of product damage and costly recalls. One of our electronics packaging customers was dealing with a 7% rate of returned products due to warped shrink wrap that exposed circuit boards. After upgrading their tunnel’s insulation, that return rate dropped to less than 1%, saving them hundreds of thousands of dollars in returns and rework annually.
At the end of the day, the importance of proper insulation in a shrink tunnel boils down to consistency. Packaging operations rely on repeatable results: every pack has to look the same, every line run has to hit production targets, and every dollar has to be spent wisely. Insulation is the quiet component that makes all of that possible. It’s not as flashy as a new conveyor or a digital temperature controller, but without it, even the best tunnel won’t perform at its peak.
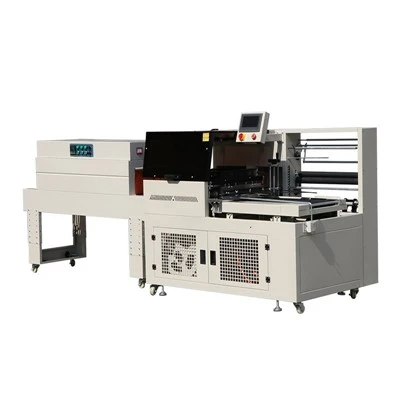
If you’re noticing higher film waste, fluctuating shrink quality, rising energy bills, or minor line worker accidents around your shrink tunnel, it’s time to check your insulation. We’re here to help—whether you need a full insulation audit, custom replacement panels, or guidance on maintaining your existing insulation to keep your shrink tunnel running efficiently for years. Don’t let a small insulation issue turn into a big expense for your operation.
Smart Packaging Systems References:
Packaging Machinery Manufacturers Institute. (2022). Industrial Shrink Tunnel Efficiency Report.
National Institute for Occupational Safety and Health. (2021). Workplace Heat Safety in Industrial Packaging Operations.
Film and Packaging Association. (2023). Shrink Film Compatibility and Heat Profile Guidelines.
Langfang Huanqi Machinery Equipment Co., Ltd.
As one of the most professional shrink tunnels & accessories manufacturers and suppliers in China, we also support customized service. Please feel free to buy advanced shrink tunnels & accessories for sale here from our factory. Quality products and reasonable price are available.
Address: No. 40, Row 11, North Side of Central Street, Wangpeizhuang Village, Pingshu Town, Dacheng County, Langfang City, Hebei Province
E-mail: huanqijixie@outlook.com
WebSite: https://www.huanqiwrap.com/
